 EVERY ORDER SUPPORTS FAMILIES IN NEED


Updated 0 comments
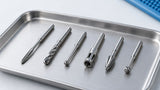
A dental bur is a rotary cutting instrument that fits into a dental handpiece and is used to cut, shape and polish tooth structure, restorations and bone. Among all the tools in the profession, burs are definitely high on the list - and there are a lot of them. The good news is that every dental bur can be described by five key specifications: material, shank, head shape, grit or blade design, and size. Learn those five and dental bur catalogues - and ISO codes - become much easier to read.
In this guide we break each one down, with the sizing tables we get asked about most. Bookmark it - it's the reference we use ourselves.
Anatomy of a Dental Bur
Every bur has three parts: the shank, which fits into the handpiece; the neck, the narrow section that carries the head; and the head, the working end that touches the tooth. Think of it this way - the shank decides which handpiece you're working with, the head shape and size decide what the bur does, and the grit (diamond) or blade count (carbide) decides how aggressively it does it.

Shank Types: FG, RA, HP, Long and Short Shank
The shank is the longest part of the bur and the part that goes into the handpiece, so it's chosen by handpiece, not by procedure. Get this one wrong and the bur simply won't seat - or worse, it seats and runs out of true. Here are the ones you'll meet:

| Shank | Full name | Shank diameter | Typical handpiece category | Typical use |
|---|---|---|---|---|
| FG | Friction grip | 1.6 mm | High speed (air turbine or electric) | Cavity and crown preparation, enamel and ceramic cutting, finishing. The most common shank. |
| FG long shank | FG surgical / extra long | 1.6 mm, 20 mm and longer total length | High speed | Endodontic access, posterior molars, surgical sites, deep cavities. Longer reach, same head. |
| FG short shank | FG mini / pediatric | 1.6 mm, typically 16 mm total length | High speed, mini heads | Children, limited mouth opening, posterior access with small handpiece heads. |
| RA | Right angle (latch type, CA) | 2.35 mm with latch groove | Slow speed / contra-angle | Caries removal, polishing, finishing, endodontics, surgical bone work. |
| HP | Handpiece (straight) | 2.35 mm, 44.5 mm total length | Straight handpiece (laboratory or surgical use) | Laboratory work, denture and acrylic adjustment, some surgical procedures. |
Always follow the bur manufacturer's recommended RPM: the permissible speed varies with head diameter and instrument design.
The ISO shank codes you will see most often in catalogues: 313 = FG short (under 18 mm), 314 = FG standard (18–20 mm), 315 = FG long (20–23 mm), 316 = FG extra long (23 mm and up), 204 = RA standard (about 22 mm), 205 = RA long, 104 = HP standard (44.5 mm).
In the shop: FG diamond burs · all diamond burs · long shank and RA burs are filtered by shank in each collection.
Materials: Diamond, Carbide, Steel, Gold
Dental burs are made from different materials, and every material has its own advantages - so most of us keep more than one kind in the tray.
Diamond burs remove material by abrasion rather than by fluted cutting edges. Diamond grit is electroplated or sintered onto a steel blank. They're especially effective on hard, brittle materials such as enamel and ceramics, with dedicated diamond instruments commonly used for zirconia adjustment. They're the instrument for crown preparation, veneer preparation, adjusting ceramics and any enamel work.
Carbide burs cut with blades machined from tungsten carbide. Carbide burs use defined cutting blades, which can produce very smooth surfaces on dentin and restorative materials - particularly when higher-flute finishing burs are used. They are the choice for cavity preparation, caries removal, finishing composite and trimming acrylic. Blade count matters: 6–8 flutes cut, 12–20 finish, 30 polishes.
Steel burs are the cost-efficient option. They're more flexible than diamond or carbide, so they're less likely to snap, but they dull quickly and are prone to corrosion. Mostly slow-speed caries removal and lab use.
Finally, gold diamond burs. These are premium diamond instruments, and in Eagle's gold bur range the highly homogeneous spread of the diamond is designed to give smoother work with less vibration, a lower operating temperature, higher durability and a better surface finish. For the full diamond-versus-carbide argument, we wrote it up separately: diamond vs carbide burs.
Head Shapes and ISO Shape Numbers
If the shank is about the handpiece, the head shape is about the job. There are dozens of shapes, and each one exists because a specific preparation needed it. These are the ones a general practice reaches for every day, with the ISO shape number you'll see in every manufacturer's code.

| Shape | ISO shape no. | Common sizes | Use |
|---|---|---|---|
| Round | 001 | Carbide ¼–8; diamond 008–050 | Caries removal, cavity opening, endodontic access |
| Inverted cone | 010 | Carbide 33½–39; diamond 009–018 | Undercuts, retention grooves, flattening cavity floors |
| Pear | 237 / 238 / 239, depending on geometry | Carbide 330 (short), 245 (long) | Cavity preparation - the 330 and 245 are the standard prep burs |
| Cylinder, flat end | 108–111 | Diamond 008–018 | Shoulder margins, axial walls, occlusal reduction |
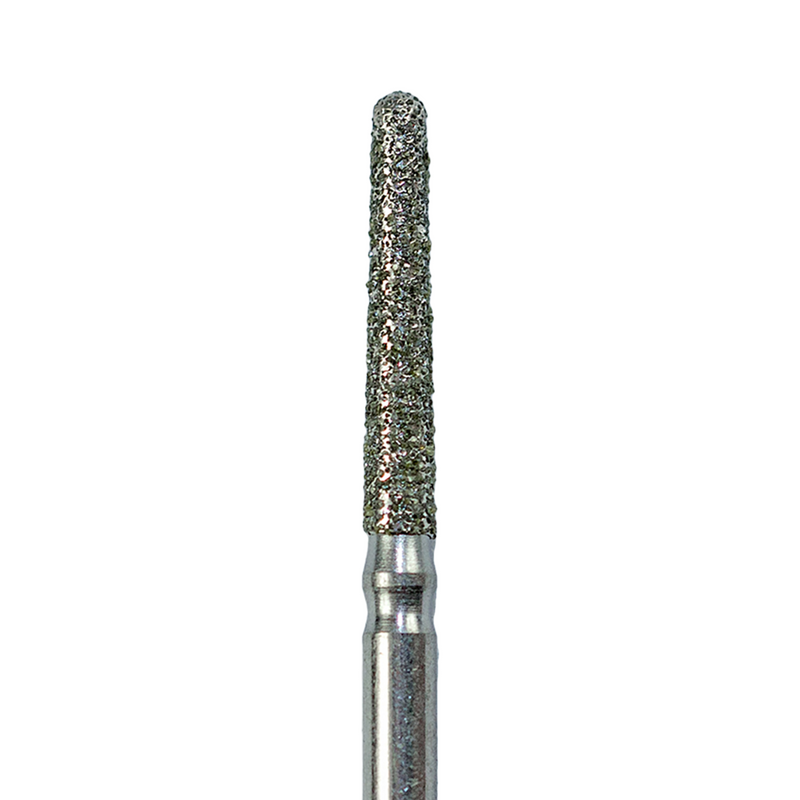
| Cylinder, round end | 138–142 | Diamond 010–016 | Chamfer margins, crown preparation |
| Tapered fissure | 169–173 (flat end), 196–199 (round end) | Carbide 169–172; diamond 010–027 | Crown preparation, cavity walls, crown removal |
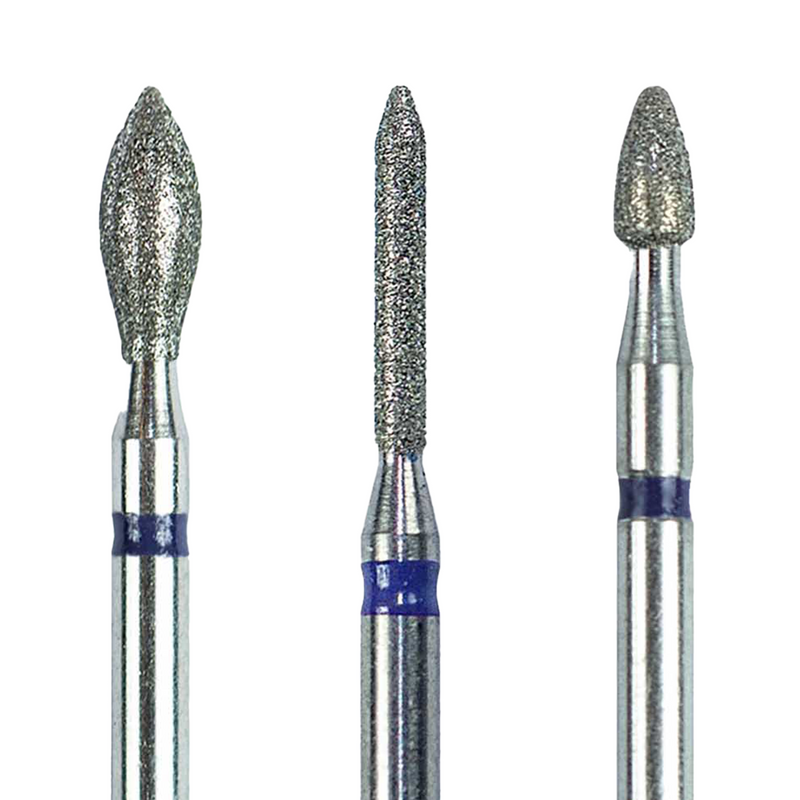
| Flame / ogival | 247–250 | Diamond 010–018 | Interproximal and lingual reduction, veneer preparation, finishing |
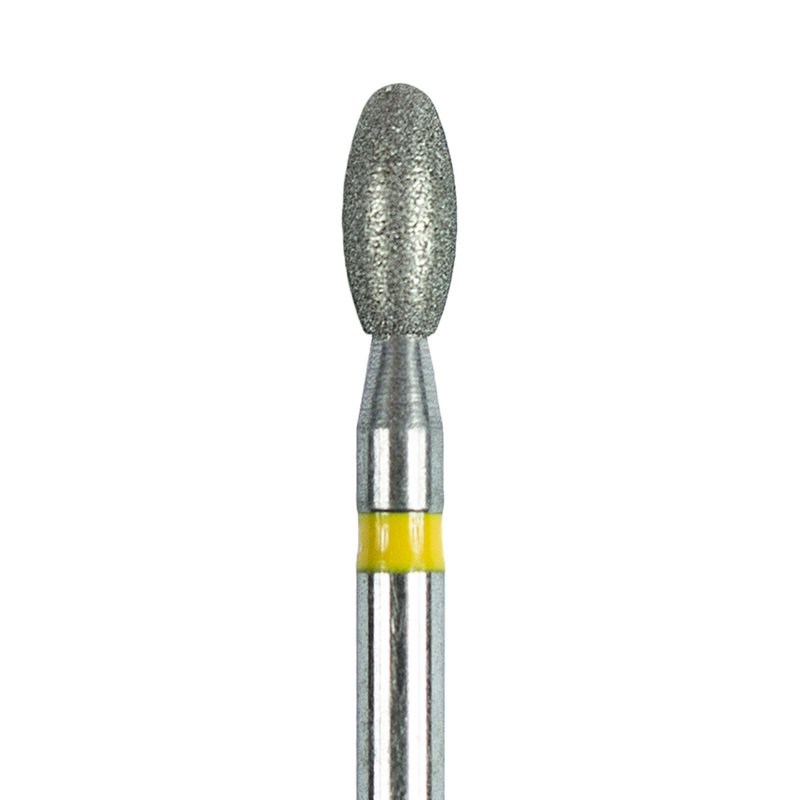
| Egg / football | 257 (football) / 277 (egg) | Diamond 014–032 | Lingual reduction of anteriors, occlusal adjustment |
| Needle | 164–166 | Diamond 010–016 | Interproximal access, fine contouring, IPR |
| Wheel | 041 / 042 | Diamond 030–050 | Lingual reduction, occlusal grooves |
One question we get constantly: 330 or 245? Both are commonly used pear-style carbide burs, but the 245 has a longer working head, so it reaches deeper in the same preparation. Exact head dimensions vary slightly between manufacturers, so check the specification on the product page.
Grits: What the Colour Bands Mean
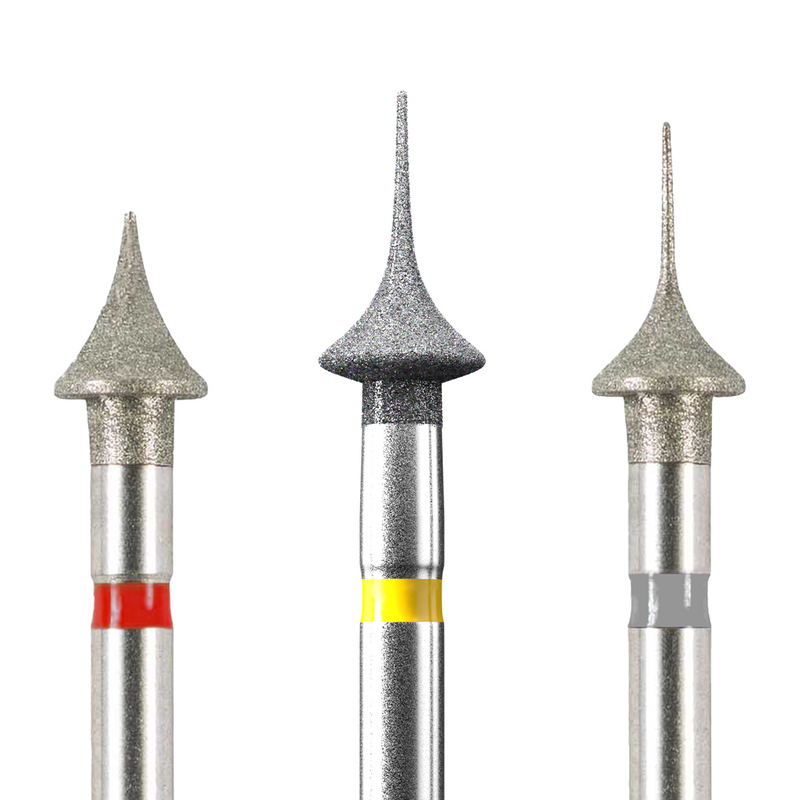
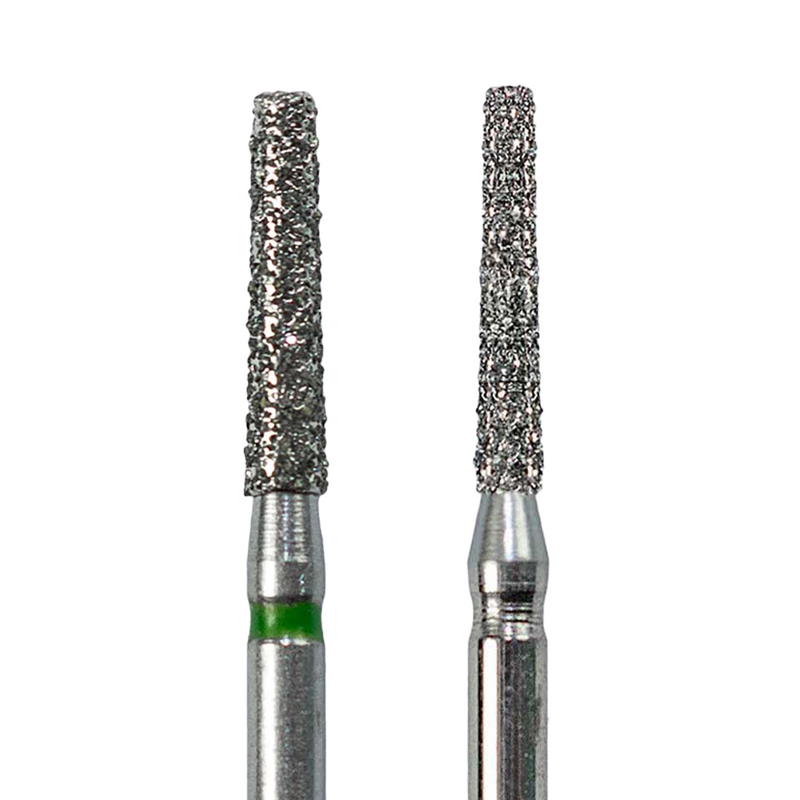
Every diamond bur carries a coloured band on the shank, and that band is the grit. Coarse grit removes material fast and leaves a rough surface; fine grit is for finishing. In a typical crown preparation you'd run green for the bulk reduction, a plain unbanded medium or red for the margins and refinement, then yellow or purple to finish. Once you know the colours you never need to read the label.

| Band colour | Grit | ISO code | Particle size (approx.) | Use |
|---|---|---|---|---|
| Black | Super coarse | 544 | 180–250 μm | Rapid bulk reduction, crown removal, zirconia sectioning |
| Green | Coarse | 534 | 150–180 μm | Bulk reduction, crown and bridge preparation |
| No band | Medium | 524 | 107–120 μm | General preparation - medium grit carries no coloured band |
| Red | Fine | 514 | 50 μm | Margins, finishing preparations, composite finishing |
| Yellow | Super fine | 504 | 30 μm | Final finishing, polishing enamel and ceramic |
| Purple | Extra extra fine | 494 | 15 μm | High-gloss finishing of composite and porcelain |
Carbide burs are classified by blade number and cutting geometry rather than diamond grit. Some manufacturers use coloured bands to distinguish cutting and finishing carbides, but unlike diamond grit colours, carbide colour coding is not universal - always check the manufacturer's specifications.
Sizes: Reading Head Diameter
Diamond burs make this easy: the last three digits of the ISO code are the head diameter in tenths of a millimetre. 010 is 1.0 mm, 012 is 1.2 mm, 014 is 1.4 mm, and so on up through 016, 018, 021 and 023. Carbide burs are less kind - they use the older US numbering, where one number identifies shape and size together. Here are the two families you'll look up most:
| Round carbide no. | Head diameter | Inverted cone carbide no. | Head diameter |
|---|---|---|---|
| Round ¼ | 0.5 mm | Inverted cone 33½ | 0.6 mm |
| Round ½ | 0.6 mm | Inverted cone 34 | 0.8 mm |
| Round 1 | 0.8 mm | Inverted cone 35 | 1.0 mm |
| Round 2 | 1.0 mm | Inverted cone 36 | 1.2 mm |
| Round 4 | 1.4 mm | Inverted cone 37 | 1.4 mm |
| Round 6 | 1.8 mm | Inverted cone 39 | 1.8 mm |
| Round 8 | 2.3 mm | - | - |
How to Read a Dental Bur ISO Number
ISO 6360 gives every bur a 15-digit code in five groups. It looks intimidating on the box, but it's the same five groups every time. Take a typical FG round diamond, 806 314 001 524 014:
- 806 - head material: galvanically bonded diamond (500 = tungsten carbide, 330 = steel)
- 314 - shank: standard FG shank, 1.6 mm diameter, approximately 19 mm overall instrument length (313 = FG short, 315 = FG long, 204 = RA, 104 = HP)
- 001 - head shape: round
- 524 - grit: medium (534 = coarse, 514 = fine, 504 = super fine; the middle digit identifies the grit)
- 014 - maximum head diameter: 1.4 mm
Manufacturers also print a short order code built from the same pieces: shape, head diameter, then a grit letter. For example, 546-016F is shape 546, a 1.6 mm head, fine grit (F = fine, M = medium, C = coarse).
Carbide burs use the same overall ISO structure, but the fourth group describes the cutting-blade or toothing design rather than diamond grit. In everyday practice, carbide burs are also commonly identified by traditional numbers such as 330, 245, 557 and 699. Once you can decode the five groups, every manufacturer's catalogue reads the same, which is exactly why the search box at the top of our site takes ISO numbers.
Choosing Dental Burs: A Short Checklist
- Match the shank to the handpiece - FG for the turbine, RA for the contra-angle, HP for the straight handpiece.
- Choose material by what you are cutting - diamond for enamel, ceramic and zirconia; carbide for dentin, amalgam, composite and acrylic.
- Choose shape by the preparation - round for access, pear and inverted cone for cavity form, cylinders and tapers for crowns, flames and needles for interproximal work.
- Sequence the grits - coarse to reduce, fine to finish. One bur rarely does both well.
- Buy ISO-coded burs from a manufacturer you can trace. A bur that runs out of true or dulls after two preparations costs you far more in chair time than it saved at the checkout. Ours are made in Israel, ISO 6360 coded, and every product page shows the code - that's how we'd want to buy them too.
Frequently Asked Questions
What do dental bur numbers mean?
The ISO 6360 code is 15 digits in five groups: head material, shank and overall length, head shape, grit or blade characteristic, and maximum head diameter. Carbide burs are also commonly identified by traditional numbers such as 330, 245, 557 and 699.
What is the difference between FG and RA burs?
FG (friction grip) burs have a smooth 1.6 mm shank and are used in high-speed handpieces. RA (right angle, latch type) burs have a 2.35 mm shank with a latch groove and are used in slow-speed contra-angle handpieces.
What do the colours on diamond burs mean?
The coloured band on the shank shows the diamond grit: from black (super coarse) through green (coarse), no band (medium), red (fine) and yellow (super fine) to purple (extra extra fine). Coarse grits reduce quickly, fine grits finish.
What is the difference between a 330 and a 245 bur?
Both are commonly used pear-style carbide burs. The 245 has a longer working head, so it reaches deeper in the same preparation. Check the manufacturer's specification for exact dimensions.
What does 014 mean on a dental bur?
It is the maximum head diameter in tenths of a millimetre, so 014 means a 1.4 mm head.
What does ISO 314 mean?
314 is the ISO code for a standard FG shank: 1.6 mm shank diameter and approximately 19 mm overall instrument length.
Where to Go Next
That's the five specifications. For an overview of bur categories by procedure, read types of burs in dentistry. For the diamond-versus-carbide decision in detail, diamond vs carbide burs. For how many uses a diamond bur gives before replacement, diamond bur lifespan. And when you know the code you need, browse diamond burs or search by ISO number in the box at the top of the page.


0 comments